Why Material Tolerances Belong in Every Adult Diaper Specification
A material tolerance is the permitted deviation around a stated target, such as basis weight, particle size, film thickness, or elastic recovery, paired with the test method used to check it. An adult diaper specification that names materials and nominal values but omits tolerances lets a factory ship components that are technically “as specified” yet behave differently from the approved sample. For procurement, quality, and product development teams working with OEM/ODM suppliers, that gap is where batch-to-batch drift, disputed shipments, and unexplained leakage complaints usually begin. This article explains which materials need tolerances, how to set limits that can actually be enforced, and how to connect them to change control, QC reports, and RFQs.
What Is a Material Tolerance in an Adult Diaper Specification?
A usable material tolerance has four parts: the property being controlled, the nominal target, the permitted range around that target, and the method, sampling, and conditioning used to measure it. If any part is missing, the limit cannot be verified, and a dispute over whether a shipment conforms has no objective answer.
Compare two ways of writing the same requirement:
Nominal only: “ADL, 45 g/m².”
With tolerance: “ADL, 45 g/m² nominal, permitted range agreed from validation data, measured by a named method and edition, with a stated number of readings per roll.”
The second version can be audited. The first can only be argued about.
Method editions matter. ISO 9073-1:2023 specifies a method for determining the mass per unit area of nonwoven fabrics, and its ISO listing shows that it replaced the withdrawn 1989 edition. A specification that cites “ISO 9073-1” without an edition leaves it unclear which procedure applies.
Vague quote language creates the same problem earlier in the process. Phrases such as “standard nonwoven” or “same as sample” leave room for drift. Buyers comparing suppliers should use a structured method like breaking down an adult diaper OEM quote by materials, GSM, packaging, and yield before negotiating limits.
Why Can the “Same Material” Still Produce a Different Diaper?
A grade name describes a family of materials, not a single measured result. Three mechanisms explain how a diaper built from nominally identical components can still change.
Variation inside a grade. Every material lot has a natural spread. If the specification sets no range, the supplier decides how much spread is acceptable, and the buyer discovers the answer only when performance shifts.
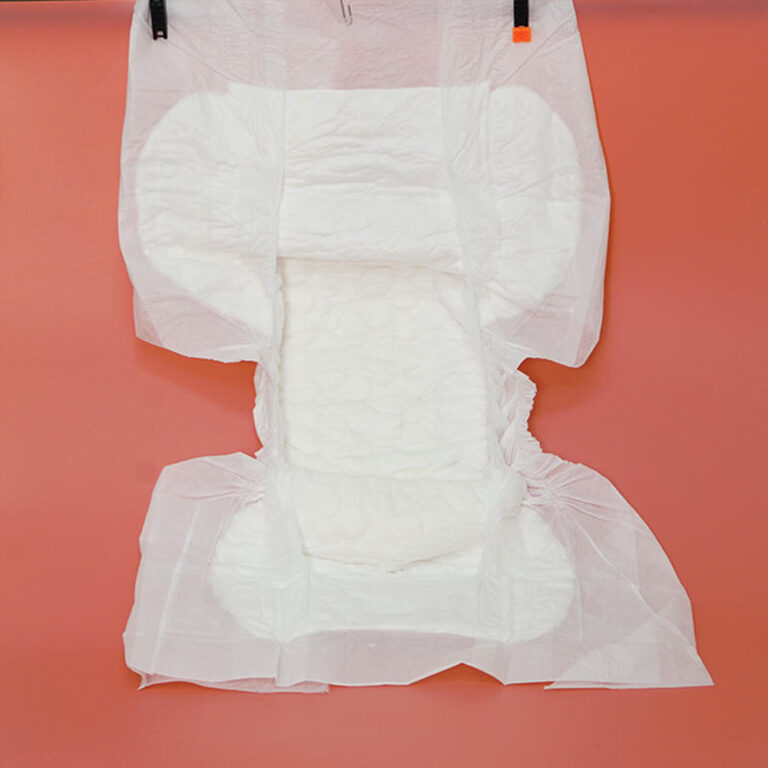
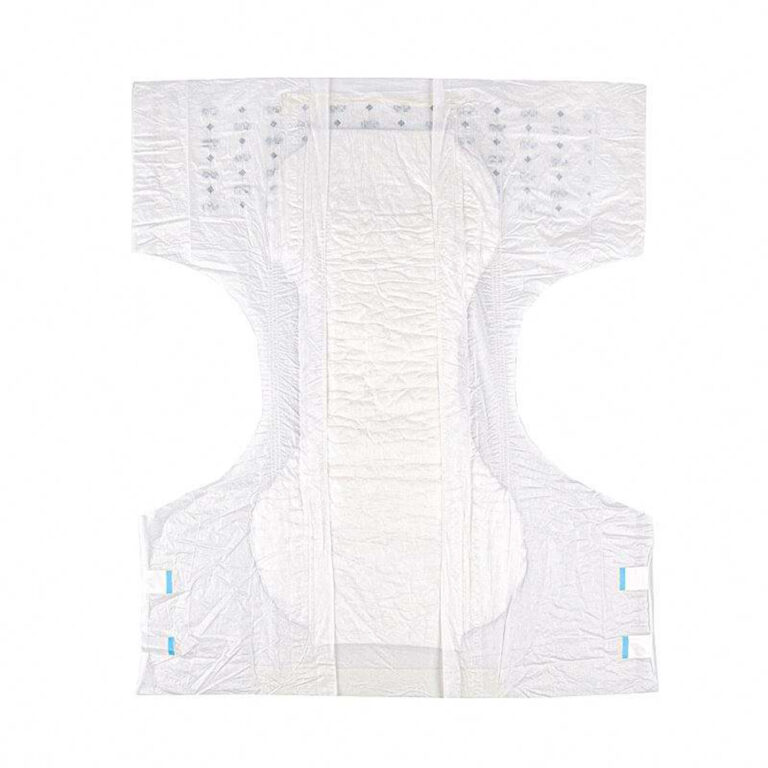
Layer interaction. An adult diaper is a fluid-management system in which topsheet, acquisition-distribution layer (ADL), fluff pulp, superabsorbent polymer (SAP), backsheet, and elastics influence one another. A deviation that is harmless in one layer can matter when it coincides with a deviation in the next. The analysis of how material changes affect adult diaper performance shows how individual layers connect to intake speed, rewet, hydrostatic resistance, and core stability.
Properties that a single number cannot capture. Basis weight is easy to specify and easy to measure, but it does not describe pore structure, compression recovery, or the durability of a hydrophilic finish. An ADL can meet its weight target and still feed liquid into the core differently. The discussion of acquisition layers in adult diapers, fast intake versus fluid distribution makes the point that GSM alone does not answer pore-size distribution. It also notes that a matching width, color, and weight does not prove an “equivalent” ADL.
The practical conclusion: a tolerance on basis weight is a starting point. It must sit alongside tolerances or acceptance limits on the properties that actually drive performance.
Which Adult Diaper Materials Need Tolerances?
Start with the components whose variation changes intake, retention, dryness, leakage, skin contact, or structural integrity. The table below lists the parameters worth controlling and the failure each one guards against. The test-method column names only method families that appear in the EDANA/INDA Harmonized Nonwovens Standard Procedures table of contents, which was marked as last updated in June 2026. Where that list has no matching procedure, the method must be agreed between buyer and supplier.
Aged-sample results, not only fresh-sample results
This table gives the parameters and method families. It does not give numerical limits, because suitable limits depend on product type, user profile, core design, and line capability. A daytime pull-up and an overnight bedridden-care brief should not share one set of numbers.
Where Tolerance Gaps Do the Most Damage
SAP: Headline Capacity Is Not a Specification
SAP is a component where a single headline figure can mislead a purchasing team. A grade with a higher free-swell number may look efficient enough to justify a lower dose per diaper. Yet swelling rate, absorbency under pressure, and particle-size distribution decide whether liquid reaches the whole core or stalls at the loading point.
The same EDANA/INDA list contains separate procedures for particle-size distribution, free swell, retention after centrifugation, and absorption against pressure. That separation is useful to buyers: each describes a different behavior, and a specification that controls only one leaves the others open.
Verify with the supplier: the SAP producer and grade, the per-lot certificate of analysis, and the dose per diaper including its tolerance. A dose that varies from unit to unit changes retention capacity independently of the SAP grade.
Nonwovens: Weight Is Necessary but Not Sufficient
For topsheet and ADL, pair the basis-weight tolerance with a performance-linked property. For topsheets, strike-through time and wetback tell you whether the hydrophilic finish works on the delivered lot. For ADLs, record fiber composition, thickness, and finish alongside weight, and treat any change in those as a change request.
Elastics, Tapes, and Adhesives: Control Function, Not Just Dimension
These parts are rarely visible in a quote, yet they decide whether cuffs hold their shape and tabs stay closed. Tolerances here are mostly functional: elongation and recovery for elastics, peel and shear for tabs, and add-on weight and bond strength for adhesives. Request aged-sample results, because recovery and bond strength can change after storage.
Why a Tighter Tolerance Is Not Automatically Better
The common assumption is that tighter limits always mean better quality. That holds only under certain conditions, and three of them are frequently missed.
The limit must fit the material supplier’s process capability. If the natural spread of a nonwoven line is wider than the limit, the supplier must sort, scrap, or price the risk. Neither outcome is free. The cost reaches the buyer in the unit price or in silent screening that no one documents.
The limit must be measurable with the repeatability the method offers. A tolerance narrower than the test method’s repeatability and reproducibility cannot be policed reliably, because acceptable material will fail and defective material will pass depending on which laboratory runs the test. Research on finished-product testing shows why this matters. A 2019 study by Cottenden and Macaulay evaluated test methods across six laboratories, using in-use leakage data from 55 nursing-home residents. It found that ISO 11948-1:1996 showed good repeatability and reproducibility and reasonable correlation with in-use data, yet proved blind to the effects of leg cuffs that gave measurable benefits in real use.
That finding supports two conclusions. A repeatable measurement can still miss a design feature, so material tolerances do not replace finished-product testing. And a method that works in several laboratories is a better basis for a contractual limit than one that only the factory can run.
Tight limits belong where function is at stake. A practical approach is to tier the specification:
Controlled tightly: properties tied to intake, retention, leakage, skin contact, or safety, such as SAP behavior, hydrophilic finish performance, ADL structure, and tab strength.
Controlled to a normal range: properties that affect handling or feel, such as nonwoven basis weight in less critical zones.
Recorded, not rejected: informational values that help trace drift without triggering rejection.
This keeps the specification credible and prevents suppliers from treating every limit as negotiable.
How Do Tolerances Connect to Change Control and QC Reports?
Tolerances only protect a buyer when they appear in three documents that refer to each other.
The product requirement and technical specification. A good adult diaper product requirement document defines what the product must achieve and how it will be verified. The technical specification then translates those requirements into material grades, dimensions, tolerances, and test procedures. If the requirement says “rewet below the agreed limit” but no material limits exist, the supplier can meet the letter of the requirement with unstable inputs.
Change control. A tolerance defines what counts as a change. A new supplier, a different grade, or a parameter outside its range should trigger formal review rather than a purchasing decision. The framework for managing raw material substitution during adult diaper supply shortages separates performance-defining materials from supporting ones. For the former, it requires laboratory comparison and line validation. Without written limits, no one can say whether a replacement is within the approved range or outside it.
The QC report. Limits are worthless if reports show only “pass.” Ask for target, tolerance, individual readings, mean, minimum, maximum, and result for each controlled characteristic, as outlined in the guide to what an adult diaper QC report should include. Reported averages can hide underfilled or out-of-range units, whereas individual readings show whether the process is stable.
What Does a Missing Tolerance Look Like in Practice?
The following scenario is hypothetical and is included only to show the mechanism.
A brand approves a golden sample whose specification lists the ADL as “45 g/m² through-air-bonded.” No thickness, fiber blend, or finish limits are written. Several months later the factory changes ADL lot source. The new roll meets the weight target, the report says “ADL: pass,” and visual inspection finds nothing. In use, third-dose intake is slower and rewet increases. No clause was breached, because the specification never described the properties that changed.
The correction is not a heavier ADL. It is a specification that freezes the fiber composition, thickness, finish, and supplier grade. It also sets acceptance limits for repeated-dose intake and rewet on the finished product, and requires approval before any substitution.
What Should Buyers Specify Before Requesting a Quote?
A quotation is only comparable when every supplier prices the same limits. Before sending an RFQ, prepare the following:
Component list with nominal values: topsheet, ADL, core materials, backsheet, elastics, tapes, adhesives, and packaging.
Parameter, range, method, and edition for each controlled property, marked as tight, normal, or recorded.
Sampling and conditioning rules for incoming material and for finished product.
Document requirements: certificates of analysis per lot, and raw-data QC reports rather than summaries.
Finished-product acceptance criteria with full test conditions, including liquid, dose volume, number of doses, and interval.
Change notification rules: no change in supplier, grade, or process without written approval, plus retained samples.
Golden sample and reference materials held by both parties.
Tighter limits can affect price, lead time, and minimum order quantities, so raise them at the quoting stage rather than after sampling. Ask each supplier to mark any limit it cannot meet and to state its typical process range, instead of accepting the whole table without comment. A supplier that answers with data is easier to evaluate than one that answers “no problem.”
Frequently Asked Questions
What is a material tolerance in an adult diaper specification?
It is the permitted deviation from a stated target for a component property, such as nonwoven basis weight or SAP particle size, together with the method used to measure it. Without both range and method, the limit cannot be verified.
Which adult diaper materials should have tolerances first?
Start with performance-defining materials: SAP, ADL, topsheet nonwoven, backsheet film or laminate, elastics, adhesives, and tapes. These directly affect intake, retention, leakage, and structural integrity. Packaging and printed items can follow with lighter controls.
Is a GSM tolerance enough to control nonwoven quality?
No. Basis weight does not describe pore structure, thickness recovery, fiber blend, or the durability of a hydrophilic finish. Pair a GSM range with performance-linked properties such as strike-through time, thickness, and composition records.
Who should set the tolerance, the buyer or the manufacturer?
Both. The buyer defines the performance the product must achieve. The manufacturer and its material suppliers provide process-capability data. Validation trials then confirm that limits are achievable and relevant to finished-product performance.
How are material tolerances checked during production?
Through lot-level certificates of analysis, incoming-material inspection, in-process checks, and QC reports showing individual readings. Slower laboratory tests may run periodically or after any supplier, material, or process change.
What happens if a material falls outside tolerance?
The lot should be quarantined and reviewed. Options are rejection, rework, or a documented deviation approved by the buyer, with traceability to affected batches. Silent acceptance by the factory defeats the purpose of the limit.